What is vacuum die casting?
Vacuum die casting degas cavity and sleeve to produce high intensity and high quality products.
Especially for high standard airtightness of car parts, it is important and necessary technique.
Root reason and solution of die casting NG product
All NG products are caused by three factors as below.
01Steam explosion caused by lubricant remains
Water from lubricant may cause steam explosion when meet molten metal. Later, adiabetic compression ( overheat ・peeling・soldering) happens too.
Solution
After spray of lubricant, the surface temperature of mold is above130.
02Adiabetic compression and oxidation reaction caused by gas inside cavity.
- Gas from air of cavity or lubricant remains caused adiabetic compression(overheat, peeling, soldering).
- Injection speed slows down caused by adiabetic compression.
- Oxidation of molten metal.
Solution
Do vacuum suction of cavity.
03Injection speed slows down by adiabetic compression which caused by gas from air of sleeve .
Injection speed slows down by adiabetic compression which caused by gas from air of sleeve and chip grease.
Solution
Do vacuum suction of sleeve.
Vacuum rank of JIS
According to Japan JIS, vacuum degree can be divided to five ranks(revised on Sep. 2021)
Vacuum rank of JIS
Low vacuum:Lower than atmospheric pressure but higher than 102Pa.
Medium vacuum:Lower than 102Pa but higher than10-1Pa.
High vacuum:Lower than 10-1Pa but higher than10-6Pa.
Ultra high vacuum:Lower than 10-6Pa but higher than 10-9Pa.
Extremely high vacuum:Lower than10-9Pa.
Current vacuum die casting all belong to low vacuum.
Composition of vacuum system
It includes vacuum device and vacuum block( valve or chill vent)

Types of vacuum system
01Mechanical valve vacuum system
This vacuum system includes vacuum device and mechanical valve. If vacuum runner design is right, quality of product can be improved immidiately.
02Sleeve vacuum system
Making a hole on the sleeve and do vacuum suction. If adding one vacuum block on the mold can improve quality of product even better.
03Chill vent vacuum system
This vacuum system includes vacuum device and chill vent. For normal standard request product, it has good cost performance.
04EV valve vacuum system
EV valve absorbs good merits of both mechanical valve and chill vent. Only if get proper close signal, it is best option to improve quality and easy maintenance valve.
Process for vacuum system purchase
01 Selection of product
According to tons of machine and chip diameter, we choose optimal vacuum device and vacuum block.
02 Discussion of vacuum runner design
Make best vacuum runner design according to the features of product.
03 Production of vacuum system
Lead time of vacuum device is two months after PO.
Vacuum block needs about one month or three weeks.
04 Vacuum system delivery, set up, trial.
After delivery, we offer maintenance and technical support service.
Check!
Please consult with us before purchase.
We will offer optimal suggestion of vacuum system according to customers production environment.
Confirmation of vacuum trial
01Confirmation of mold installation
| Confirmation subject | Content |
|---|---|
| Confirmation of valve PL surface | PL surface of valve is higher than PL surface of mold about 0.03~0.04. |
| Hit on Bunryukoʼs sleeve | Performance is good. |
02Confirmation before production
| Confirmation subject | Content |
|---|---|
| Lubricant spray spot and time | Please make sure piston and valve of fixed side is sprayed more than 1sec. |
| Vacuum suction line | Please make sure hose is connected firmly. |
| Valve protection air line | Please make sure valve protection air is supplied during low and high speed die casting. |
03Confirmation during production
| Confirmation subject | Content |
|---|---|
| Valve protection air | During low speed ・high speed die casting valve protection air should be supplied. After intensified pressure signal is accept, this function stop supplying air. Note If this function is ON by manual operation, it cannot stop automatically. |
| Burning state of chip lubricant | During molten metal fill , whether lubricant burning is much or not(Smoke is little). |
| Clearance of valve | Whether there is clearance between valve PL surface. (Please check whether there is burring or not). |
| Valve action | When mold is opened, valve is opened at the same time. Note If valve opens a little slower, the possibility of clogging risk is high. |
| Vacuum suction action | Whether you can see white gas inside hose running (Reference:During vacuum suction, vacuum hose is shrink a little ). |
| Vacuum suction timing | Whether vacuum suction action is earlier than injection sound can be heard. |
04Appearance
| Confirmation subject | Content |
|---|---|
| Appearance of valve exhaust groove | 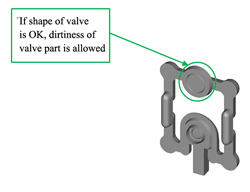 |
| Appearance confirmation(Whole) | Influence of vacuum suction can be checked |
05Others
| Confirmation subject | Content |
|---|---|
| Mold temperature | Above 120℃ |
06Die casting condition
| Confirmation subject | Content |
|---|---|
| When use vacuum valve, vacuum timing starts from 0.4 sec before low speed changes to high speed. When use chill vent, vacuum timing starts from 0.5 sec before low speed changes to high speed. When use hot chamber, after nozzle touch finished,according to different type of machine to decide vacuum delay time setting. ※Please refer to right picture | 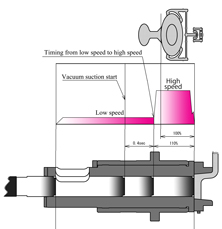 |
Vacuum Valve Attention of usage
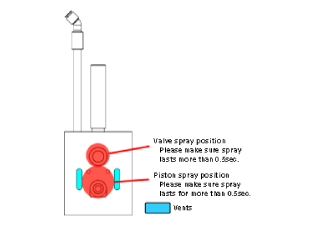
01Lubricant spray
Please make sure release agent is sprayed to the position shows below for 0.5sec.
This action can help preventing clogged valve and prolong lifespan of usage.
- Spray position of movable side
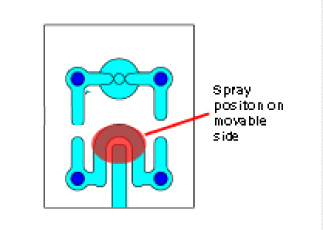
- Spray position of fixed side
02Valve installment to mold
Please make sure fixed and movable side of vacuum valve is higher than core mold about 0.03~0.08mm.
Please refer to installation drawing of vacuum valve before mold production.
Please use bolts to fix A side to mold tightly.
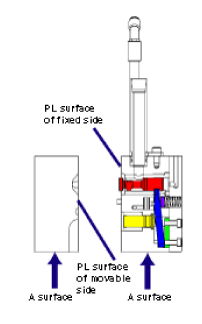
03Lubricant of sliding part
After dismantlement of vacuum valve, please make sure lubricant is sprayed on the valve・valve bush・piston・piston bush. This maintenance can decrease trouble of sliding part.
Our company recommends this lubricant for maintenance.
Our company provides free regular maintenance. Dismantle and clean vacuum valve parts is free.